A Housing, Not Just an Aluminum Bar
When you buy an LED housing profile you are buying a structural component that has to hold a metal-core PCB perfectly flat, grip a polycarbonate cover tight without buckling, run cool for tens of thousands of hours, and still look pristine under a retail showroom spotlight. We extrude it, CNC machine it and anodize it, so you can focus on building the light.
The process runs in one line: precision extrusion, in-house CNC machining, dye-controlled anodizing, and a ready-to-assemble housing at the end.
Profile Types We Extrude
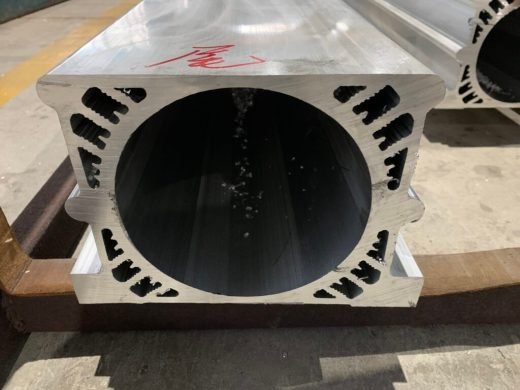
- T5 and T8 retrofit tubes: heavy-duty cylindrical housings with integrated heat-dissipating channels.
- Linear pendant and surface channels: architectural-grade profiles with seamless diffuser integration.
- Wall washers and grazers: angled housings engineered to throw light precisely while concealing the source.
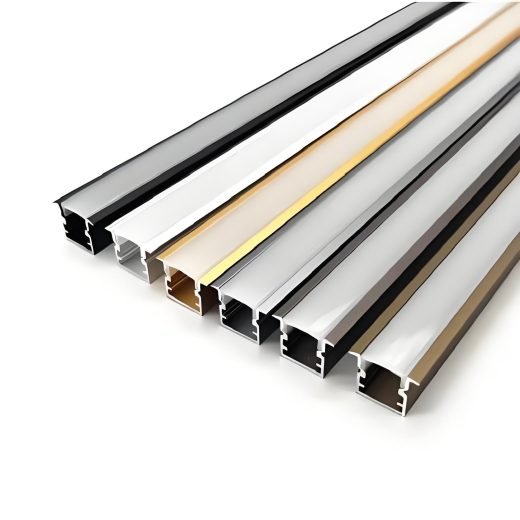
- U-channels and V-channels: ultra-slim, low-profile tracks for commercial tape light installations.
- Track light rails: robust rectangular rails with tight internal tolerances for conductive electrical tracks.
These are not generic catalog items. The snap-fit groove that holds your PC diffuser has to be dimensioned exactly to the tolerances your cover supplier molds to. The internal screw bosses must align with your molded end caps. The surface where the MCPCB sits must be flat enough to prevent the micro-gaps that trap heat and burn out diodes.
Fixing LED Burnout: Thermal Mass and Face Flatness
Early LED failure in high-wattage linear fixtures and T8 retrofits is usually a profile problem rather than a diode problem, and the pattern is consistent. The wall where the PCB sits is too thin, often 1.0 mm or less, so the aluminum saturates with heat quickly and junction temperature climbs. The extruded seating face is slightly convex or concave, so the board sits on high points with air trapped between them and heat bottlenecks at the diodes.
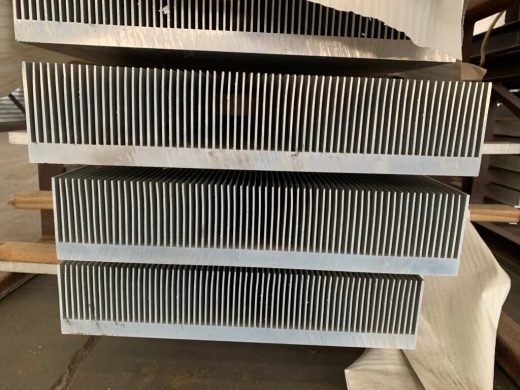
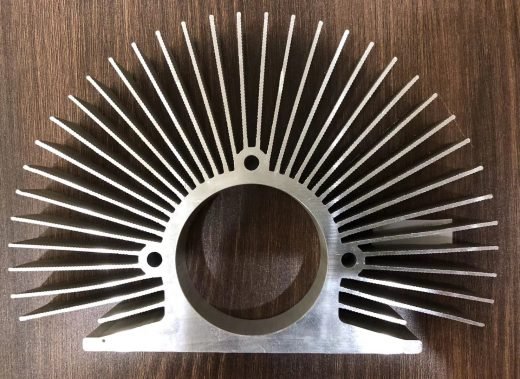
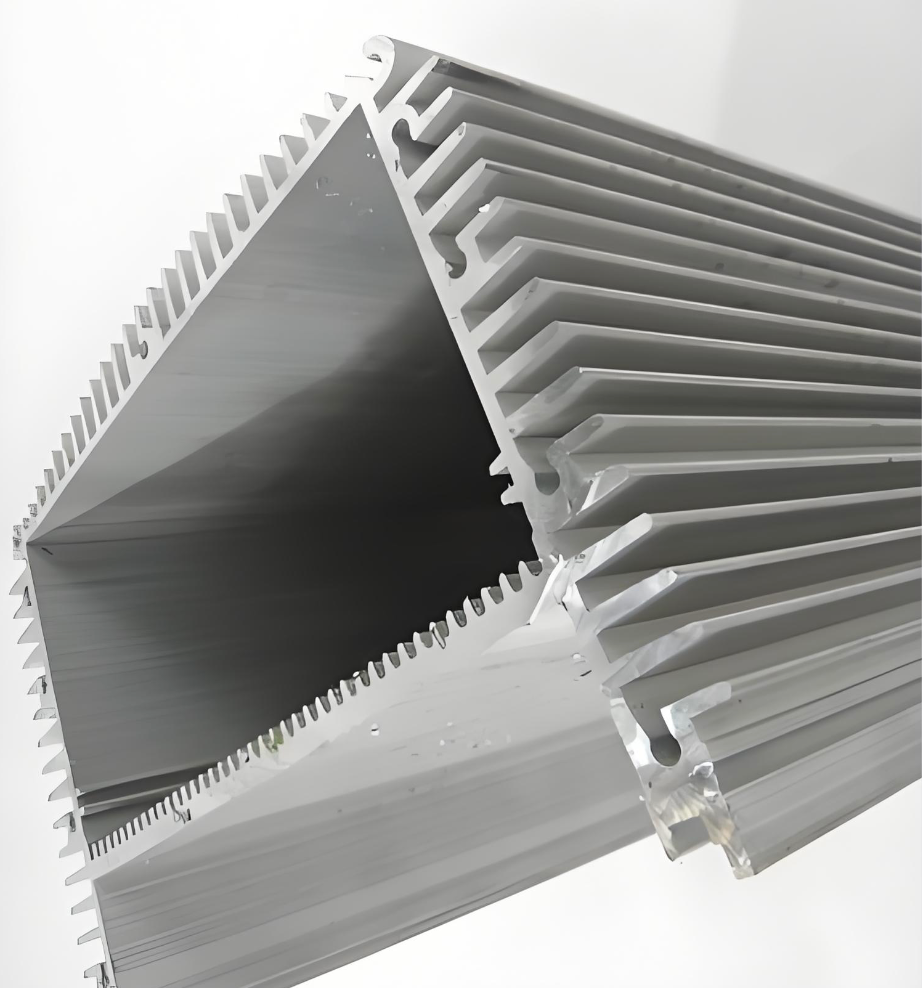
We hold the seating face flat through die design and process control, and we keep the wall under the MCPCB at a wall thickness that gives the profile enough thermal mass to spread the load before convection removes it. Where a fixture runs hot, we can also increase surface area with finned side walls that double as the visual profile.
Profile Reliability Through the Tooling
The diffuser groove is dimensioned to your cover supplier's molded tolerances, and the screw boss centers are set to match your molded end caps. We work from your fixture drawings, or, if you are still in R&D without a finalized CAD file, from your PCB width, cover type and mounting constraints. We will sketch a custom cross-section, cut the die, extrude the run, perform secondary CNC fabrication and anodize the batch in a color-matched run.
From Drawing or Sketch to Finished Housing
Send us your cross-section CAD drawing or a physical sample. If you are still in early R&D without a finalized CAD file, tell us your PCB width, cover type and mounting constraints and we will sketch a custom cross-section for your review. From there the sequence is fixed: cut the die, extrude the run, carry out secondary CNC fabrication, finish the batch in a color-matched anodizing or powder coating run, and deliver components that go straight onto your assembly line.
Because extrusion tooling costs a fraction of die casting tooling, a custom LED profile is practical even for a mid-volume fixture program. Standard length is 2 m, but most customers order pre-cut lengths matched to the fixture, which removes saw kerf loss, unusable offcuts and the floor space a saw cell occupies in a lighting factory.
Black and silver anodized housings are standard, with powder coat available where a decorative color or textured finish is required. Because every profile in an order is machined and finished together, the components in one shipment match each other in color and in dimension.
Fabrication and Delivery
Profiles are extruded in 6063-T5 as standard, which anodizes evenly and carries the thermal load of a passive LED fixture. Where a housing also acts as a structural member or has to take welding, we step up to 6061-T6. Standard length is 2 m, and we supply pre-cut, CNC drilled and tapped housings rather than raw bar, because that is how most customers order. Send the fixture drawing with cut lengths and hole positions and we ship components ready for your assembly line.
Minimum order is 500 kg, and production runs under an ISO 9001:2015 quality system.
 Industrial Aluminum