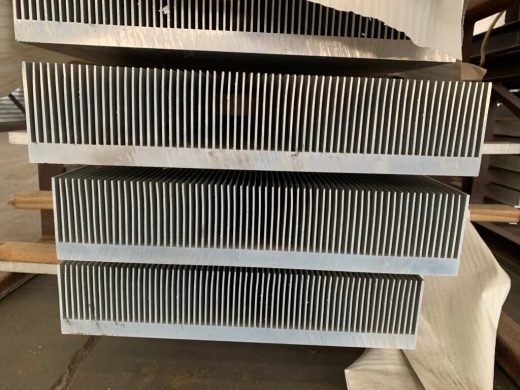
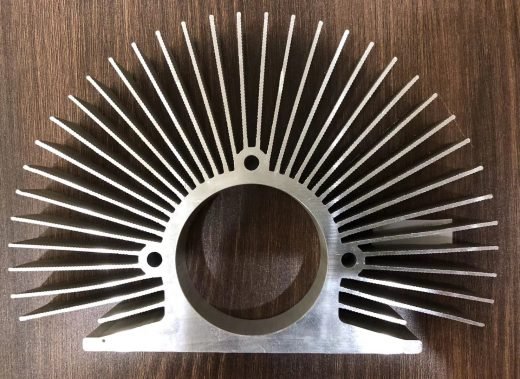
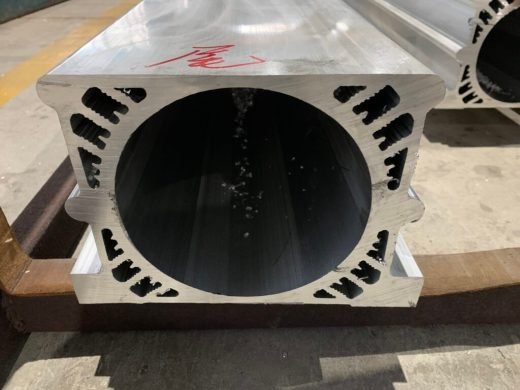
Profiles Engineered for LED Fixtures
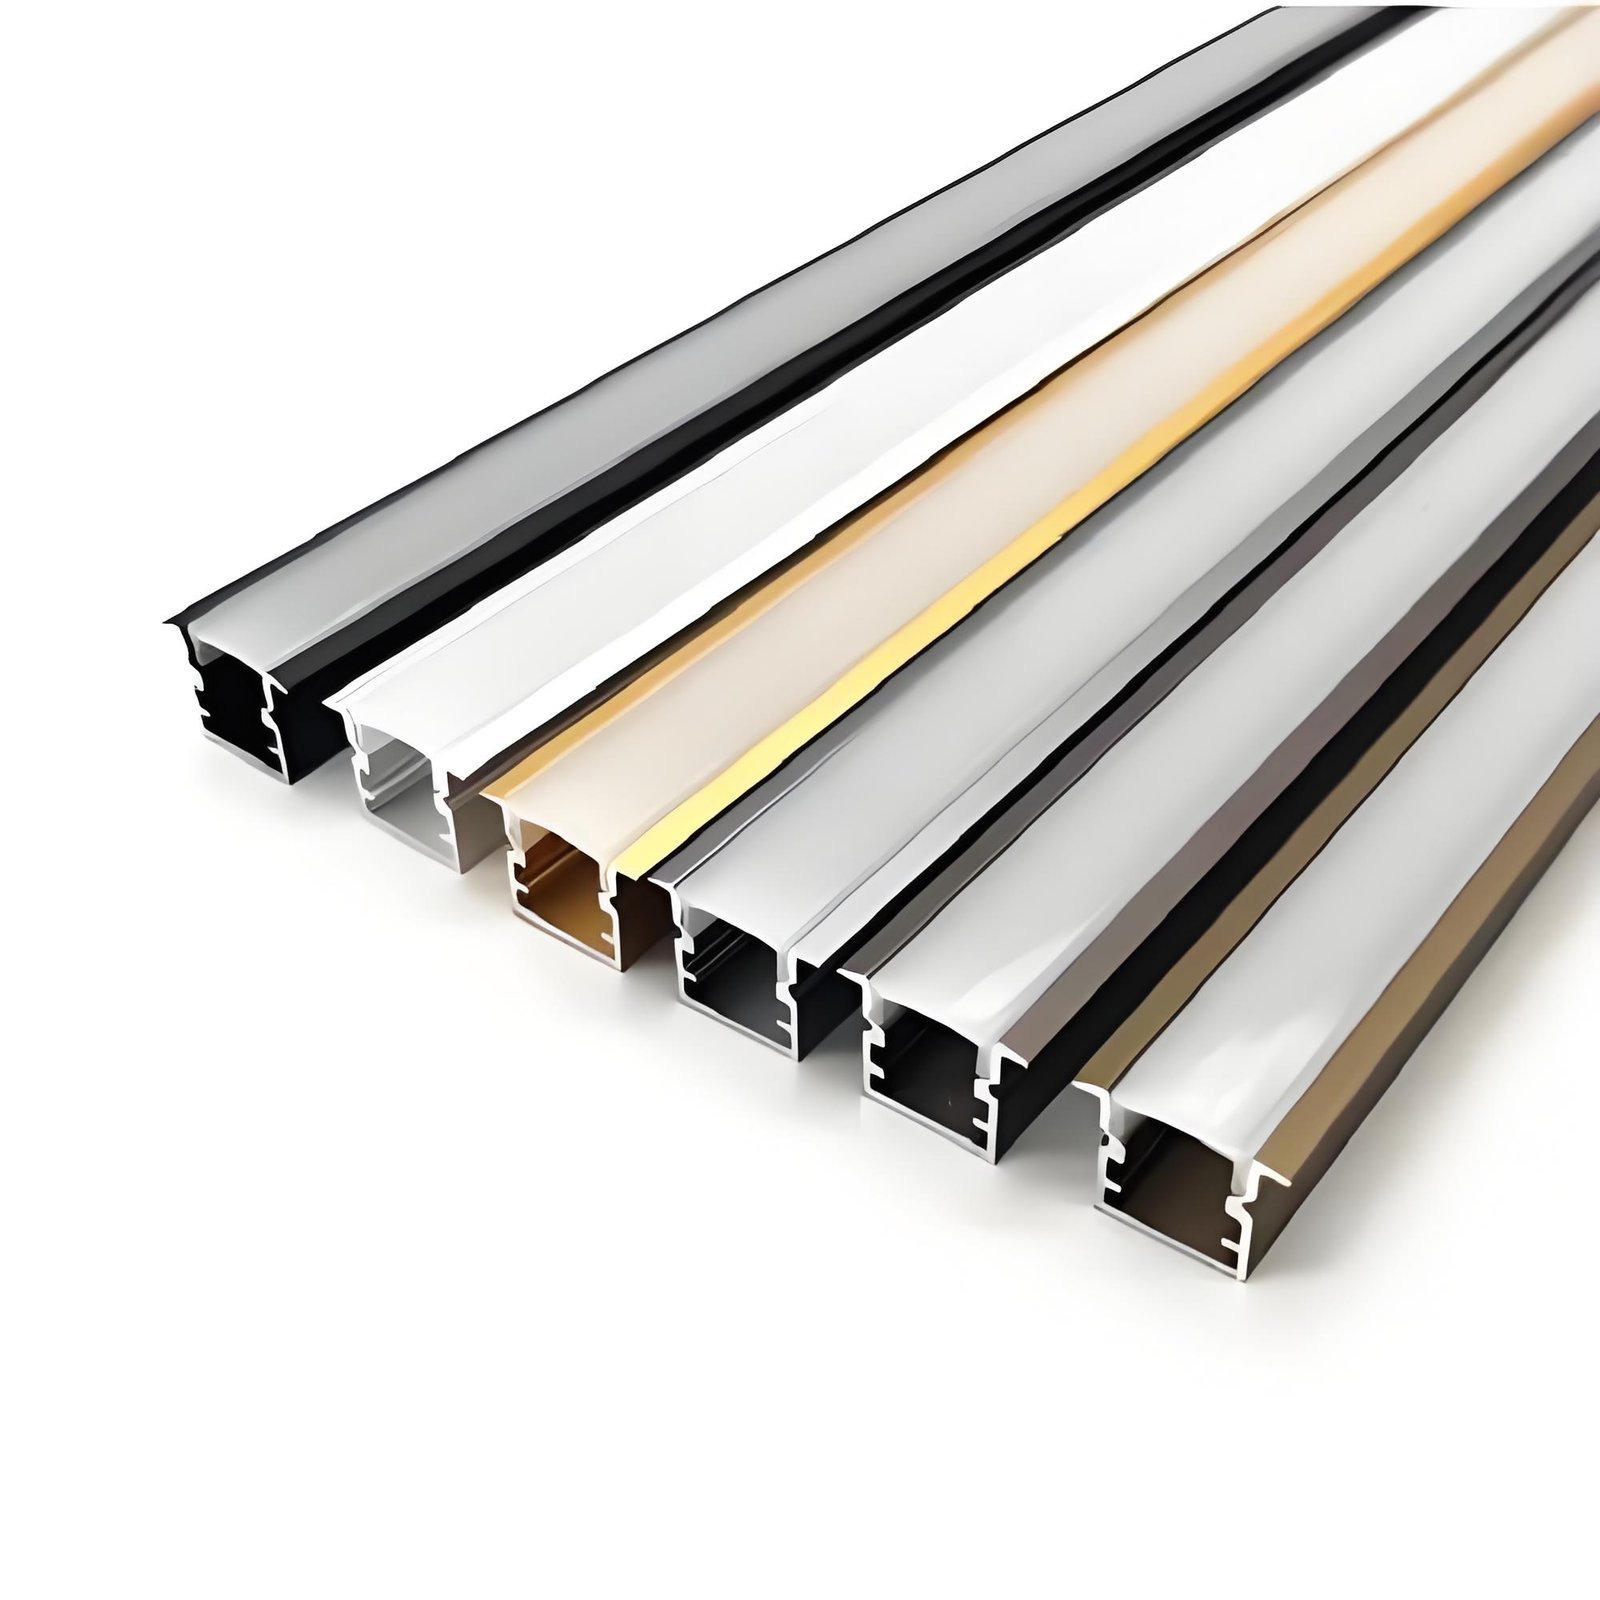
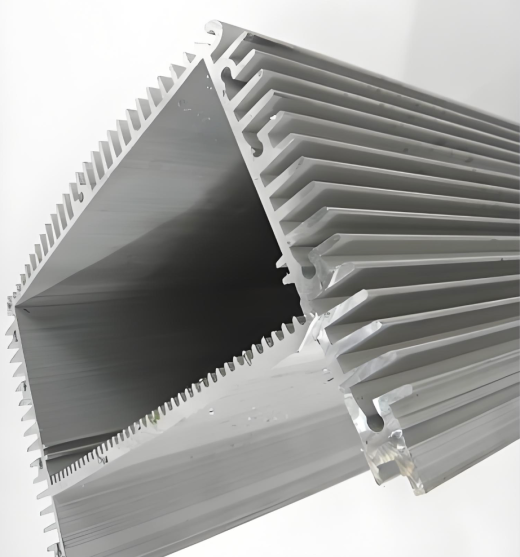
We extrude, machine and finish custom aluminum profiles specifically for the LED lighting industry. Send us a cross-section CAD drawing or a physical sample. We cut the die, extrude the profile, cut bars to your exact fixture lengths, CNC drill and tap the mounting holes, anodize or powder coat the entire batch, and ship ready-to-assemble components to your factory.
The profile you receive is the profile you designed, with your groove dimensions, your wall thicknesses and your screw boss locations. We do not push a standard off-the-shelf die when a fixture needs custom engineering.
Anodizing Color Consistency Between Batches
The most common late complaint in LED housings is color drift. A lighting company orders a batch of black anodized housings, everything looks right, and six months later a reorder shows up slightly warmer or slightly greyer on the same ceiling. The cause is almost never the anodizing line on the day of production. It is that the two batches ran weeks or months apart, on different shifts, with small differences in dye concentration, tank temperature, current density or billet chemistry. Any one of those shifting a few percent changes the final tone of black.
Every profile in your order, regardless of how many cross-sections or lengths it contains, is extruded from the same billet heat and anodized in the same tank run. For reorders we keep a physical master sample and the Lab values from the first production batch, run a short trial piece and match it before committing the full run. If you are switching suppliers, send a sample of your current housing and we will match it.
Thread-Milled End-Cap Holes
An LED housing has blind holes drilled and tapped into each end, and an end-cap screw strips there at the very end of assembly, when the PCB is already mounted and the wiring is already run. Stripped threads usually come from a worn tap cutting an undersized thread, or a blind hole too shallow so the screw bottoms out before the head seats.
We thread-mill these holes rather than tapping them. A thread mill cuts the thread profile along a helical path, producing a smoother, more consistent thread with tighter tolerance and no torn crests. We hold 6H class on every hole and set blind depth to your screw length plus at least 2 mm of clearance. Where a fixture has a removable end cap for driver access, we can install stainless steel wire thread inserts at the factory so the screw threads into hardened steel for the life of the fixture.
Diffuser Groove Fit, Verified With Your Cover
The groove that holds the polycarbonate or acrylic diffuser is the most critical dimension on an LED housing. Too narrow and the cover bows or will not seat. Too wide and it rattles, leaks light or falls out in transit. We hold groove opening to 0.15 mm on both width and depth, but the real check is physical: before the die is finalized we ask for a short sample of the cover you use, extrude a trial section and snap the cover into it. If the fit is too stiff, too loose or does not click, we adjust the groove in the die. During production the groove is gauged on a sample from every 50 bars, so drift from die bearing wear is caught early.
Straightness Over Long Fixture Lengths
A 1.5 m linear light on a wall or ceiling shows a bow immediately. The human eye picks up a 2 mm deviation over that length. Profiles leave the press with internal stress, and if it is not relieved the bar looks straight when cut and bows later as the stress relaxes. Every profile passes through a tension stretcher after extrusion, pulling the material past yield by 1 to 3% permanent elongation to equalize internal stress. We hold straightness at 0.5 mm per meter or better, and every bar is rolled on a flat inspection table before packing. For housings 2.5 m and longer we check section rigidity at die design and recommend wall thickness adjustments if the section would be too flexible.
Cut to Fixture Length: The Hidden Cost of Cutting In-House
Buying 6 m bars and cutting in-house looks cheaper per meter, but add the kerf loss from every saw cut, the offcuts too short to use, bars scrapped because the saw was not square, the labor hours feeding a saw instead of assembling fixtures, and the floor space. A lighting factory using 10 tons of aluminum a month at a 5% sawing scrap rate discards 500 kg of finished, anodized aluminum every month. We supply profiles cut to your exact fixture lengths at 0.1 mm, with no kerf loss, no offcuts and no miscuts.
Ordering
Machining and finishing cover precision cut-to-length at 0.1 mm, CNC thread-milled end-cap holes at 6H class, CNC-drilled mounting holes at 0.15 mm position, the verified PC cover groove, silver or black anodizing in a single batch with powder coat or PVDF available, in-line PE film, and packaging by fixture type and length or kitted one fixture per pack. Minimum order is 500 kg on a new die, or 200 kg from an existing die.
 Industrial Aluminum