Powder Coated Aluminum Window and Door Frame Profiles
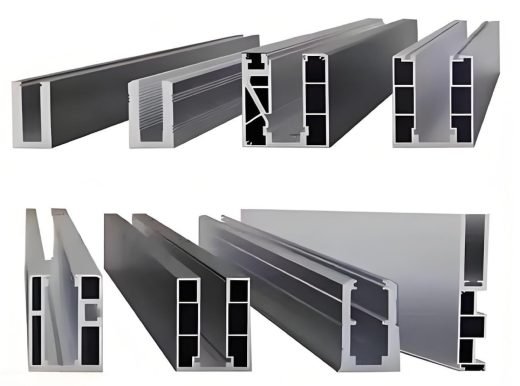
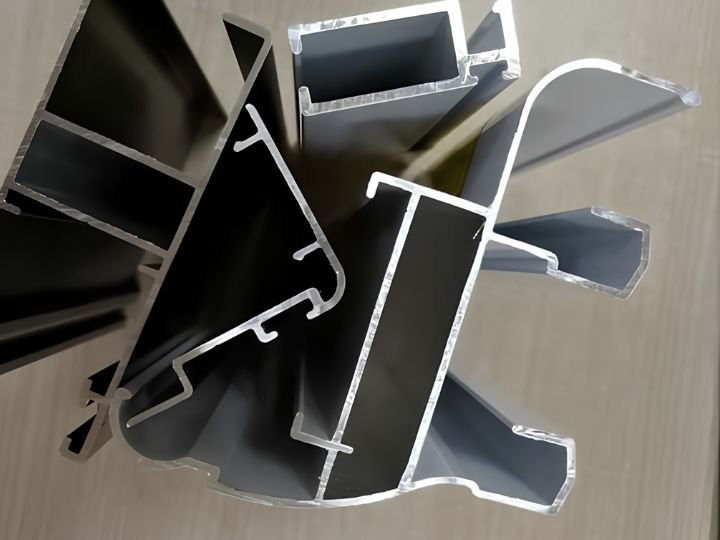
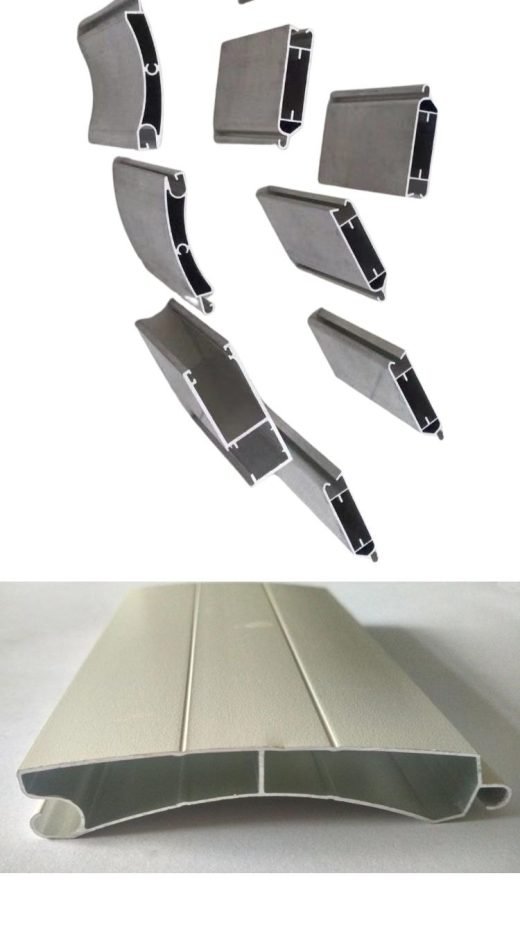
From blueprint to finished frame, we produce 6063-T5 architectural profiles by hot extrusion and finish them with powder coating on our own line. The profiles are made for window and door brands that need a frame to arrive already finished: outer frames, sashes, mullions, transoms, thermal break sections, glazing beads and sub-frames, all extruded to drawing and coated to the color you specify.
More than twenty years in aluminum extrusion has taught us where the problems hide. A section that looks right on a drawing can be impossible to crimp at the corner, or too thin at the screw boss so the fixing strips out. Our engineering team reviews every die design before it is cut so those issues are settled on paper rather than on your assembly line.
Optimized Mechanical Performance
Webster hardness is held at 10 ±2 HW. That band gives frames the rigidity to carry heavy glazing without visible deflection under wind load, while keeping the alloy ductile enough to prevent cracking during high-speed punching and corner crimping. Thermal break profiles are produced with a polyamide barrier so the frame separates the warm inner face from the cold outer face, which reduces heat loss and keeps condensation off the interior surface.
Weatherproof Coating and Color Control
Powder coating is applied electrostatically and cured in an oven, producing a continuous film that blocks moisture and oxygen from reaching the aluminum. We use established powder brands such as AkzoNobel and Tiger. Adhesion is rated Grade 0, salt spray testing runs to at least 1000 hours without corrosion, and the coating is formulated for more than ten years of color retention without chalking under UV exposure.
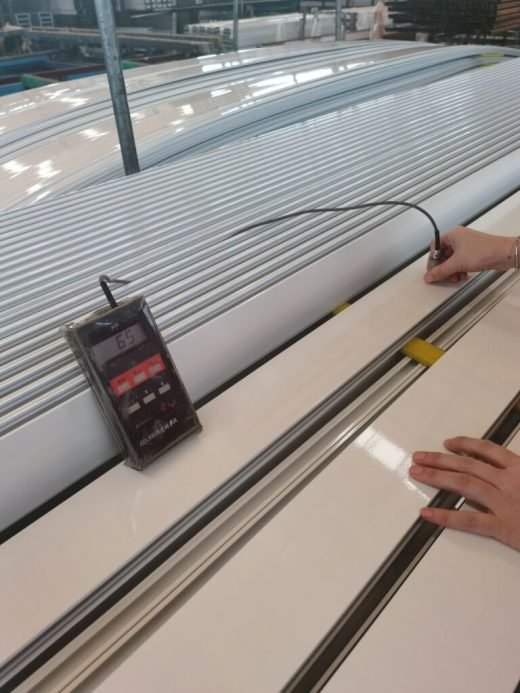
Coating thickness is normally 60 to 80 µm and can be adjusted on request for a heavier build or a specific specification. RAL color matching is available, with textured and metallic finishes offered alongside the standard range. Because the profiles in an order are pretreated, sprayed and cured together, the outer frame, sashes and trims arrive as one consistent color rather than as three close-but-not-identical tones.
Tight Tolerances on Assembly Dimensions
Critical assembly dimensions are controlled within ±0.2 mm and the profiles are produced to GB/T 5237 high-precision tolerances. The purpose of that discipline is straightforward. Gaps between frame and sash are where drafts and noise enter, and where drained-and-ventilated systems fail if the drainage path does not line up. Holding the mating dimensions close eliminates rattle after assembly and helps the finished window meet its energy efficiency and sound insulation targets without shimming on site.
OEM and ODM Development
We accept DWG, STEP and PDF files for new profile development. Every mold design is reviewed for manufacturability before cutting, which reduces the risk of a design-to-production discrepancy appearing after the die is already made. Deep processing is available alongside extrusion: precision cutting, punching, tapping and milling, so you can receive parts that go straight to assembly rather than lengths that still need several operations.
Traceable Quality and Lead Time
Traceability runs from raw aluminum ingot spectral analysis through to final film thickness and color difference measurement, so a queried batch can be checked against its own records rather than against a generic specification sheet. Die and mold manufacture takes around 10 to 15 days, with production following in about 15 to 20 days. Standard lengths are 5.8 to 6.0 meters, minimum order quantity is 500 kg per profile, and profiles are packed in brown paper for surface protection in transit.
Send your drawings and the exposure conditions the frame has to live with, and we will confirm alloy, coating grade and color before anything is cut.
 Architectural Aluminum