Anodized Aluminum Window and Door Frame Profiles in 6063-T5
Anodizing is not a coating applied on top of the metal. It is an electrochemical conversion of the aluminum surface itself. The profile is made the anode in an acid electrolyte, and a dense oxide layer grows out of the substrate and into it, so there is no interface where a film can lift or peel. That is why anodized aluminum window and door frames keep their appearance in coastal air, in polluted city centers and on buildings that are washed rarely, if ever.
We run an in-house anodizing line, which means the film thickness, the color and the surface texture are controlled under one roof instead of being subcontracted. For window and door brands, that matters for a simple reason: the frame is the part of the window the customer sees every day, and a color that drifts between production runs is a complaint waiting to happen.
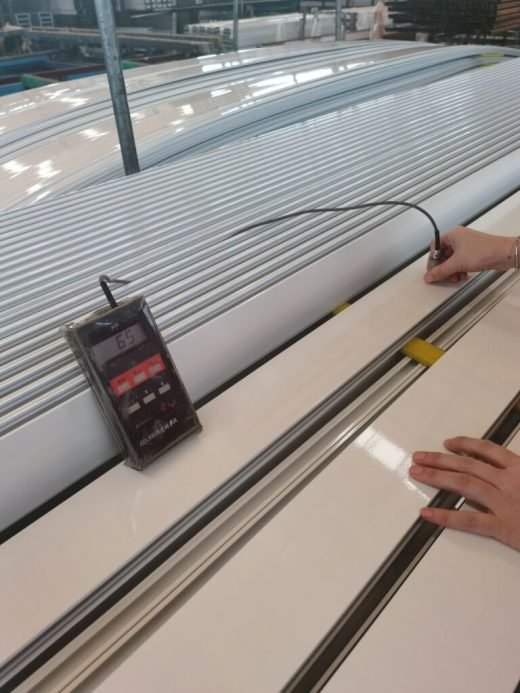
Film Thickness Control: 10 ±2 µm as Standard
Our standard anodic film is 10 ±2 µm, and running our own line lets us hold that band tightly rather than averaging out of a wide range. For more demanding exposure, the layer can be built up to 15, 20 or 25 µm on request. The difference is not cosmetic. A thicker oxide layer takes proportionally longer to break down under salt and humidity, which is why a thickened film is the normal specification for facades within a few hundred meters of the sea.
Corrosion performance tracks that thickness. Standard 10 µm profiles are tested to at least 500 hours of neutral salt spray, and thickened films extend that beyond 1000 hours. The exact figure that applies to your order is stated on the inspection report for the batch that ships.
Strength and Workability: Webster Hardness 10 ±2 HW
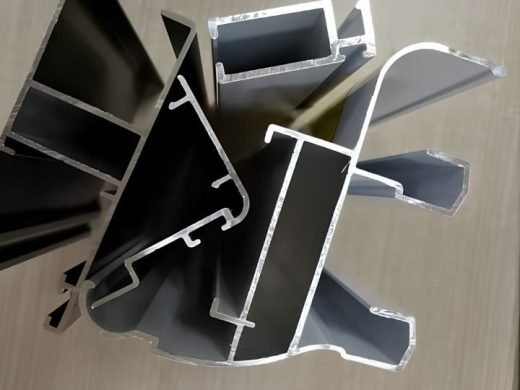
Window and door frames are fabricated, not just installed. Profiles are sawn to length, punched for hardware, crimped at the corners and screwed through. A frame that is too soft deforms under the crimping die and will not hold a miter closed; one that is too hard cracks at the corner or dulls tooling faster than the fabricator can tolerate. Holding Webster hardness at 10 ±2 HW keeps the profile rigid enough to carry heavy glazing and ductile enough to survive high-speed punching and corner crimping without cracking.
Colors and Textures
Anodizing produces its color through the oxide layer rather than through pigment, and the range covers silver, champagne, bronze and black. Because the finish is integral to the metal, it keeps a metallic depth that paint and powder cannot reproduce, and the surface stays conductive and weldable in the areas left unsealed. Color consistency between profiles in the same order is controlled by processing the frame set together, so a casement outer frame, its sash and the matching door threshold read as one material.
Tolerances and Fabrication
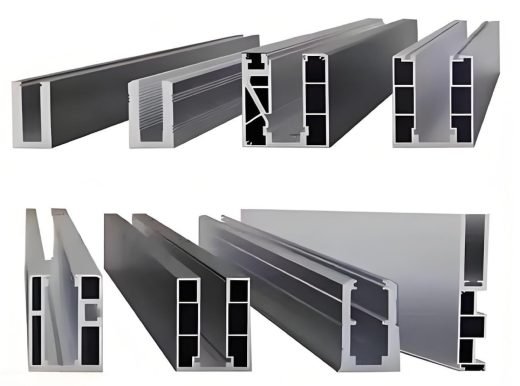
Profiles are produced to GB/T 5237 high-precision and super high-precision tolerances, with critical assembly dimensions controlled at the die. Casement window frames, sliding tracks and premium door frames all depend on the same thing: a consistent section so that hardware, gaskets and beads fit without hand-fitting on the assembly line. Cutting, punching, tapping and milling can be carried out before shipment if you would rather receive ready-to-assemble parts.
Lead Time, Packing and Ordering
Tooling takes around 10 to 15 working days, with total sampling at 20 to 25 days. Profiles are supplied in standard 6.0 meter lengths, protected in shrink film, and minimum order quantity is 500 kg per profile. Delivery can be arranged FOB or CIF depending on how your logistics are set up. Send your drawings, the color reference and the exposure class of the building, and we will confirm the film thickness and finish that suits the project.
 Architectural Aluminum