PV Frames Engineered for Automated Framing Lines
A frame that twists during lamination, pits after three monsoons, or arrives at the plant with mounting holes 2 mm off is not just a defective part, it is a warranty claim waiting to happen. On the surface a solar frame looks simple: a long aluminum profile with a groove for the laminate, a slot for the mounting bolt and a few drainage paths. In an automated framing station, small deviations turn into real bottlenecks. A subtle bow can jam the framing machine, a rushed anodizing seal fails salt spray within months, and slotted holes that drift out of tolerance force installers to re-drill on site, scratching the coating and wiping out project margin.
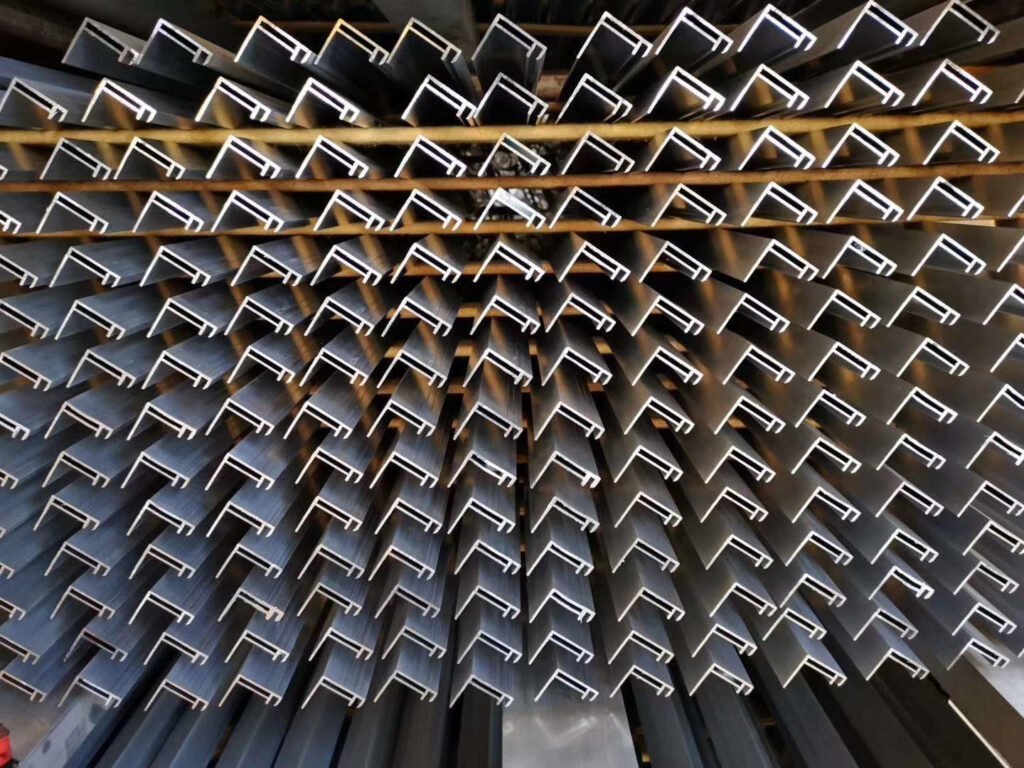
We manage the whole fabrication chain rather than just supplying the profile: precision cutting, CNC punching, drainage slotting, grounding boss integration and protective film application, so the frames arrive at your module plant ready to feed the framing machinery.
Straightness: Why Micro-Twist Causes Cell Micro-Cracks
If a profile has a slight structural twist, it forces the glass laminate into a constant, subtle curve while the silicone cures. That residual stress concentrates at the solar cell edges, and months later under environmental loading the micro-cracks propagate. The module may pass initial testing while its long-term power degradation curve steepens.
We hold profile straightness to 0.5 mm/m or better. Every profile passes through a dedicated tension stretcher after leaving the press, because roller straightening only masks internal stress rather than removing it. Cross-sections are monitored at the start and end of every production run with a profile projector, and critical dimensions touching the laminate and mounting clamps are held to 0.15 mm. For standard rooftop projects the alloy is 6063-T5; large-format utility panels and heavy snow-load zones step up to 6063-T6 or 6005-T5.
Anodizing and Sealing: Stopping White Rust
White rust on anodized aluminum is almost always a sealing problem. If the oxide pores are not fully closed, moisture and salt ions penetrate the layer and cause sub-surface corrosion, which is what happens when lines use cold-sealing additives or run billets high in iron tramp elements.
Our baseline for outdoor exposure is AA15 at 15 µm or more. For high humidity, coastal sites and floating solar, we mandate AA20 at 20 µm or more as an architectural finish. We seal with a high-temperature nickel salt hot-water process rather than a quick cold dip, validate every batch with the ISO 3210 acid dissolution test to confirm pore closure, and run a chrome-free passivation pre-treatment to arrest filiform corrosion at scratch points. Profiles are extruded from primary 6063 billet, never remelted scrap, because clean metal yields a clean oxide seal.
Hole Position and Post-Extrusion Fabrication
Misaligned tolerances stall ground-mount installations immediately. If pre-drilled frame holes miss the racking slots by a few millimeters, the crew re-drills on site, which voids the manufacturer's warranty and exposes raw aluminum to corrosion. We CNC drill or punch every mounting hole after the profile is cut to length, referencing the same datum edge across the whole batch, which keeps hole positional tolerance within 0.2 mm. Drain slots are engineered as elongated channels so water actually evacuates instead of clogging a small circular hole with dust and organic matter. Grounding marks are extruded into the die as a raised boss and pre-drilled, giving a clean flat surface for electrical contact without scraping anodizing away on site.
Surface Protection in Transit
Frames rejected for scratches are the most frustrating kind, because the extrusion itself may be metallurgically perfect. We apply heavy-duty PE protective film in-line as the profile exits the aging oven, and it stays on through cutting, punching and assembly. Saw and punch tooling uses nylon or rubber contact pads to eliminate metal-on-metal friction, and finished frames are stacked with foam or corrugated separators, stretch wrapped and loaded onto reinforced export pallets. The film peels cleanly at your assembly line.
Profile Selection and Ordering
Standard PV frames for residential and commercial modules use 6063-T5 with AA15 anodizing in silver or black. High-strength frames for large-format modules and heavy snow or wind loads use 6063-T6 or 6005-T5 with AA15 or AA20. Coastal, offshore and floating sites use 6063-T5 or T6 with AA20 and nickel sealing. BIPV, thin-film and special laminates run to specification with anodized, electrophoretic or PVDF finishes.
Engineered frame features include an integrated grounding boss extruded as a raised pad, a silicone overflow groove sized to your specified adhesive bead volume, and directional drainage slots positioned so that water evacuates at varying design tilt angles. For a completely custom profile the MOQ is 500 kg per shape; because a standard frame needs both a long-side and a short-side profile, the combined entry threshold is typically 1,000 kg. Every frame in an order is extruded from one billet batch and anodized in one tank run, so color matches across every pallet.
 Industrial Aluminum